custom 100mm cold room sandwich panels suppliers: Specification, Ordering and Quality Notes
What This Product Is and Where It Fits
Total cost of ownership shifts once returns are counted. A 100 mm panel rated for -25 °C storage carries the refrigeration load for a decade; every millimetre of core variance or facing delamination adds kilowatt-hours to the monthly bill. Buyers in food logistics, pharmaceutical cold chains, and modular build contractors specify 100 mm because it balances structural span (up to 3.6 m unsupported) with a U-value typically below 0.22 W/m²·K — without the freight penalty of 150 mm stock.
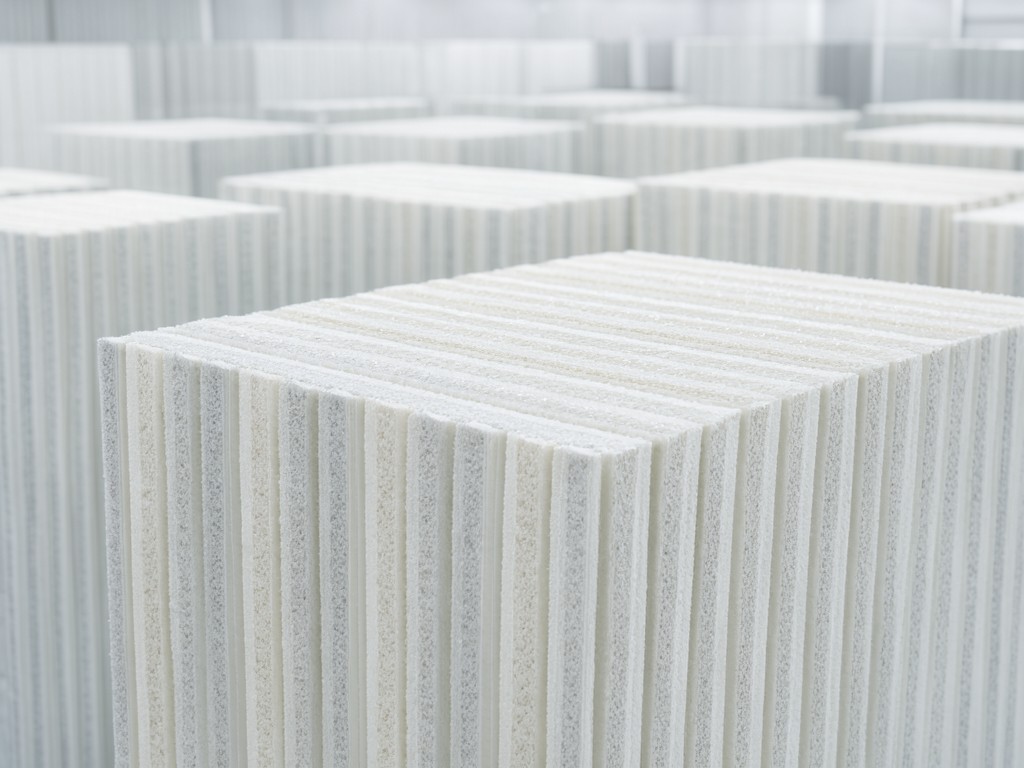
The panel ships as a finished composite: two pre-painted steel or aluminium facings bonded to a rigid polyisocyanurate (PIR) or polyurethane (PUR) core. Camlock or tongue-and-groove joints seal on site with vapour-barrier tape. No field foaming, no curing wait. That construction logic is why importers and OEM buyers treat it as a line item with a fixed lead time, not a project variable.
Where Cheaper Alternatives Fall Short
Cheaper stock options fail at the worst point in the season. Panels sourced on price alone tend to show three complaint patterns within the first 18 months: core shrinkage pulling joint tapes loose, facing corrosion at cut edges where galvanising was skipped, and thermal bowing on south-facing elevations because the core density drifted below 38 kg/m³. Each failure triggers a site visit, a partial teardown, and a warranty claim that exceeds the per-square-metre saving.
A typical 100 mm PIR panel at 40 kg/m³ core density weighs 11.2 kg/m². Drop the density to 35 kg/m³ and the panel loses 0.6 kg/m² — but the lambda value rises from 0.022 to 0.026 W/m·K. Over a 500 m² cold room running 24/7, that delta costs roughly €1,800 per year in extra compressor runtime. The payback on the denser core is under 14 months.
Material Options and Their Trade-offs
Core: PIR vs PUR
PIR (polyisocyanurate): Standard for 100 mm. Lambda 0.021–0.023 W/m·K. Chars at 300 °C, passes FM 4880/4881 without added fire retardants. Slightly higher cost per m³.
PUR (polyurethane): Lambda 0.023–0.025 W/m·K. Lower exotherm during foaming — easier on thin facings. Requires halogenated FR to meet Class 1 / B-s1,d0. Used when foam-in-place repair is specified.
Facing: Steel vs Aluminium
Pre-painted galvanised steel (0.5–0.6 mm): Standard. 25 µm polyester or 55 µm PVDF. Scratch resistance 2–3 kg pencil hardness. Weight 4.5 kg/m² per face.
Aluminium (0.7–1.0 mm): Specified for wash-down zones, coastal sites, or cleanroom partitions. No red rust risk. Lower stiffness — requires closer purlin spacing (≤ 1.2 m). Adds €8–12/m².
Specification Rule
If the project spec calls for FM 4880 approval, PIR core with 0.6 mm PVDF-faced steel is the only combination that certifies without project-specific fire testing. Substituting PUR or polyester-facing voids the listing.
How It Is Built and What That Changes
Continuous lamination on a double-belt press delivers the most consistent bond line. The facings unwind, adhesive rolls on, core foam rises in a controlled gel window, and the sandwich passes through a heated zone (140–160 °C) for 8–12 minutes. Final thickness tolerance ±1 mm. Density profile across the width stays within ±2 kg/m³.
Discontinuous (batch) presses are used for custom lengths over 13.5 m or non-standard facings (stainless, embossed aluminium). Cycle time stretches to 25 minutes per batch. Bond strength still exceeds 100 kPa shear, but the foam skin on the cut edges is thinner — requiring extra sealant on vertical joints. Tooling amortisation decides the MOQ: continuous line needs 1,500 m² to justify a colour change; batch press can run 300 m².
Camlock profiles are roll-formed into the facing before lamination. The male/female geometry locks panels vertically; horizontal joints rely on the tongue-and-groove with a butyl tape bead. Misaligned camlocks are the single most common site complaint — usually traced to a 0.3 mm facing thickness variance. We hold facing gauge to ±0.02 mm on the slitter.
How to Choose Before Requesting a Quote
Send the following with every enquiry. Missing data adds two email rounds and 48 hours to the quotation.
- Internal temperature set-point and maximum ambient (e.g., -25 °C / +40 °C)
- Clear span between structural supports — determines facing gauge and camlock type
- Fire rating required: FM 4880, EN 13501-1 Class B-s1,d0, or local code reference
- Hygiene zone classification (ISO 14644, FDA, HACCP) — drives facing finish and joint sealant spec
- Panel orientation: vertical wall, ceiling, or floor (floor panels need 0.7 mm top skin and high-compressive core ≥ 150 kPa)
- Total square metres and maximum panel length for container loading
- Port of discharge and whether pallets must be double-stacked in a 40 ft HC
A complete data set lets us confirm core density, facing system, and joint profile in the first revision. We return a marked-up drawing with panel layout, camlock schedule, and a per-square-metre price split (core, facings, adhesive, profiling, packing).
Working as a Production Partner, Not a Catalogue Supplier
Catalogue suppliers stock standard 1000 × 11500 mm panels in white polyester. That works for a distributor filling a warehouse. It fails when an OEM buyer needs 1150 mm wide panels to match a modular frame grid, or a brand manager requires a custom RAL colour with a 20 µm anti-bacterial topcoat for a retail launch in six weeks.
We allocate a production slot once the technical datasheet is signed. First-article panels (typically 3 m²) ship air-freight for dimensional and thermal verification — guarded hot-plate test at 10 °C mean temperature, result within ±3 % of declared lambda. Bulk production starts after written approval. Lead time from approval to EXW: 18 working days for continuous line, 12 days for batch press.
Changes after approval incur a re-tool charge (€350–600) and reset the clock. We document every revision in a shared change log so the importer's QC team sees exactly what shifted.
Export Packaging and Handling Protection
Panels leave the line stacked flat, alternating facing direction to neutralise bow. Each stack (max 2,800 kg) sits on three 100 × 100 mm timber bearers at 1/4, 1/2, 3/4 points. Top and bottom panels get 2 mm corrugated cardboard edge protectors on all four corners. The entire stack is wrapped in 150 µm UV-stabilised stretch hood, then strapped with two 19 mm PET bands per bearer.
| Parameter | Standard Export Spec | Optional Upgrade |
|---|---|---|
| Stack height | ≤ 2.4 m (fits 40 ft HC double-stack) | ≤ 2.1 m for single-stack air freight |
| Edge protection | 2 mm corrugated corners | 5 mm foam profile + corner boards |
| Moisture barrier | Stretch hood only | PE liner + desiccant sachets (1 kg per 10 m²) |
| Labeling | Batch ID, dimensions, weight, handling icons | Customer SKU barcode + QR link to COA |
| Container loading | Floor-loaded, bearers on container floor | Steel stillage frames (returnable) |
Double-stacking in a 40 ft HC requires the bottom stack to carry ≤ 5.5 t. At 11.2 kg/m², that limits the bottom stack to 490 m². We calculate the split per container and provide a stuffing plan with the shipping instructions.
Next Step: Request a Sample Pack
A physical sample pack contains: 300 × 300 mm cut sections of each facing/core combination quoted, camlock profile samples, joint tape, and the current batch test certificate (lambda, density, bond shear, fire rating). Packs ship DDP to your QA lab within 10 working days of receiving the signed specification sheet.
Include the project data list from the selection section. We return a priced technical submittal within 48 hours.



